
Do You Know The Reasons For The Difficulty in Making Injection Molds? The Cavity And The Core Are Three-dimensional.
Author: zhongzhu
2023-04-28
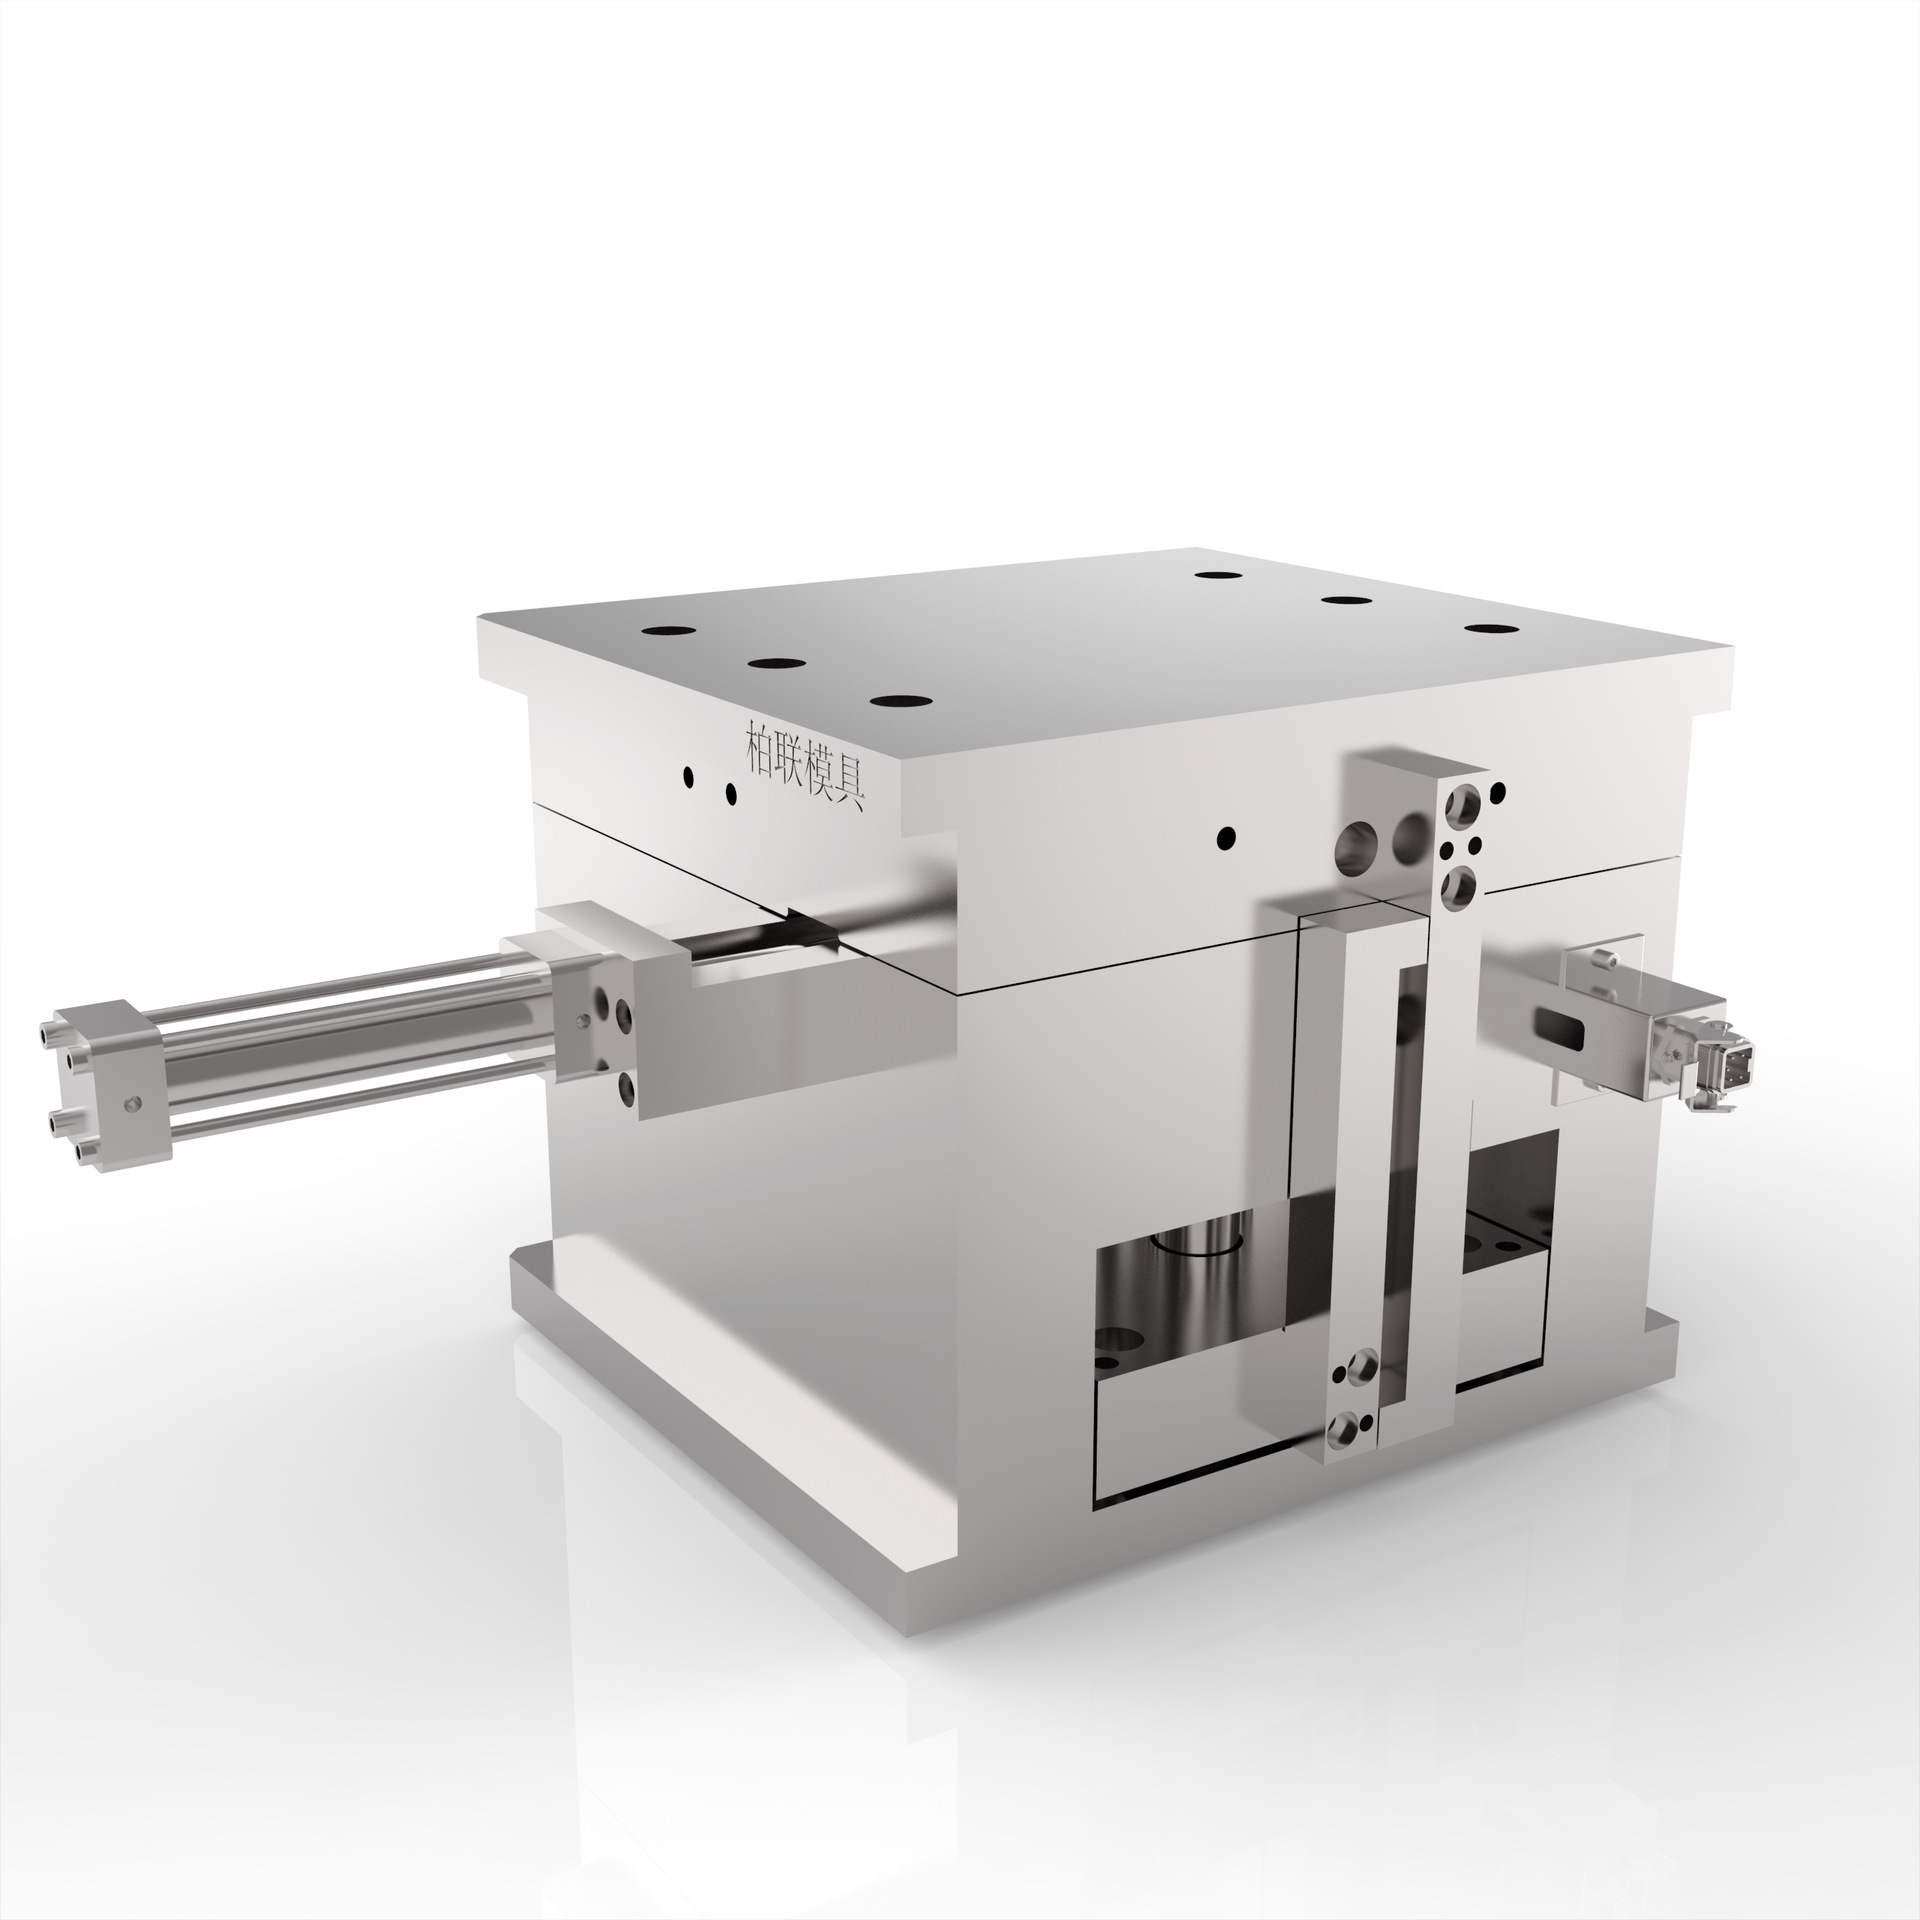
The external and internal shapes of the plastic parts are directly formed by the cavity and the core. These complex three-dimensional profiles are difficult to process, especially the blind hole type internal molding surface processing of the cavity. If traditional processing methods are used, not only It requires workers with high technical level, many auxiliary fixtures, many tools, and a long processing cycle.
High precision and surface quality are required, and long service life is required.
At present, the dimensional accuracy requirements of general plastic parts are IT6-7, and the surface roughness is Ra0.2-0.1μm. The corresponding dimensional accuracy requirements of injection mold parts are IT5-6, and the surface roughness is below Ra0.1μm.
The roughness of the recording surface of the laser disc should reach the mirror processing level of 0.02-0.01 μm, which requires the surface roughness of the mold to reach 0.01 μm or less. Long-life injection molds are necessary to improve high efficiency and reduce costs. At present, the service life of injection molds generally requires more than 1 million times.
Precision injection molds should use a rigid mold base, increase the thickness of the template, add support columns or conical positioning elements to prevent the mold from deforming under pressure, and sometimes the internal pressure can reach 100MPa.
The ejection device is an important factor affecting the deformation and dimensional accuracy of the product, so the best ejection point should be selected to make the demolding uniform everywhere. Most of the high-precision injection molds are inlaid or fully assembled in structure, which requires the machining accuracy and interchangeability of mold parts to be greatly improved.
The process flow is long and the manufacturing time is tight.
For injection molded parts, most of them are matched with other parts to form a complete product, and in many cases, other parts have been completed, and they are eagerly waiting for the supporting injection molding parts to be listed. Due to the high requirements for the shape or dimensional accuracy of the product, and due to the different characteristics of the resin material, after the mold is manufactured, it is necessary to repeatedly try and correct the mold, which makes the development and delivery time very tight.
Off-site design, off-site manufacturing.
Mold manufacturing is not the ultimate goal, but the final product design is proposed by the user. The mold manufacturer designs and manufactures the mold according to the user's requirements. In most cases, the injection production of the product is also performed by other manufacturers. In this way, product design, mold design and manufacture and product production are carried out in different places.
Professional division of labor, dynamic combination.
The production batch of the mold is small, which is generally a single-piece production, but the mold needs a lot of standard parts, ranging from a mold base to a small thimble. These cannot and cannot be completed by only one manufacturer alone, and the manufacturing process is complex, common equipment and numerical control. Equipment usage is extremely uneven.
Electroplating Process Of Plastic Products (water Electroplating And Vacuum Electroplating) There Are Two Common Electroplating Processes For Plastic Products: Water Electroplating And Vacuum Ion Plating.
MAGMA Parent Company Acquires FLOW-3D Subsidiary
Related Article

Fast sampling is the fastest way to win business in the hardware machining and plastic mold industries. Customers want a working sample in days, and a 3D printer delivers it, but only when you know how to print in 3d correctly.
how to print in 3d

Fast sampling is the fastest way to win business in the hardware machining and plastic mold industries. Customers often send an STL file and expect a working sample in days.
how to print an stl file

