
Gun Pump Manifold Switch Body Injection Mold Design and 3D drawing
1st place: One-piece die-cast rear subframe
Manufacturer: Hantmann Metal Foundry, Germany
Dimensions (length, width and height): 1260mmx670mmx390mm
Weight: 19300 grams
Alloy: Al Si 10MnMg
Product description: Highly functionally integrated, connection points for mounting control arms, struts and stabilizers, electric drives and attaching components to the body. In particular, in the die casting process, a closed cavity is created by the hollow profile integrated into the casting process, which, in combination with the topologically optimized design of the upper shell, meets all strength, stiffness and NVH requirements . The overall design of the TOP-HAT avoids complex joining processes and various single parts.
Design, casting and forming requirements: In the casting process and mold design, with the support of different simulation software, the focus is on the following characteristics: optimal filling of the entire part and partial local compression of key functional areas, optimal vacuum of the cavity Auxiliary ventilation, taking into account the reduction of material in thick-walled areas where strength is required. Optimization of machining content and contours, using special tooling technologies such as JetCooling integrated in the extrusion zone, and fixing a long cavity resulting in inserts to improve NVH behavior. The basis of the above work was done in advance: installation space studies, various operational strength analyses and calculations, topology optimization, stress and deformation calculations, development of solutions for centering and fixing of inserts, and consideration of thermal expansion and contraction.
Reasons for using a die-casting process: The integrated die-casting design avoids complex assembly steps such as welding. Different parts/components can be cancelled. Machining can be done in one set-up. Thanks to the insertion technology, weight reduction is achieved while maintaining the same or higher component performance. Therefore, the die-casting method becomes the optimal and most economical process.
Reason for award:
- Highly functional integration
- Topology optimized design combined with integrated plug-in ensures high stiffness as well as NVH requirements
Second place: SP52 lower shell
Manufacturer: BMW Plant in Lanshut, Germany
Dimensions (LWH): 1258 mm x 1152 mm x 165 mm
Weight: 30067 grams
Alloy: Al Si 10 Mn Mg
Product description: As the core component of the high-voltage storage system, the lower housing component must meet various high functional requirements throughout its service life.
Design, casting, and molding requirements: Typically, the die-cast housing for a high-pressure storage unit of this size is two-piece. To exploit the cost potential, this SP52 high-voltage storage unit features a one-piece die-cast design for the first time. On the mold side, the two-plate solution was adopted because of its advantages in circuit material, optical casting operation, mold weight and die casting machine design. In the design of the mold, special consideration is given to the following points:
- Minimum application amount of release agent
- long runners in the mold
- Heat treatment of die castings
- Weldability of die castings
- Crashworthiness of die castings
- Dimensional requirements for die castings
In addition, the tightness of the assembled HVS (no voids in the machined housing flange) also plays an important role.
Reasons for Die Casting: Compared to traditional sheet metal construction, the advantages of die casting hybrid housings are as follows:
- Reduce 16 single pieces
- The length of the sealing seam is reduced by more than 50%
- 6kg weight loss
- Significant savings in manufacturing costs
Reason for award:
- Comprehensive approach to obtain economically optimal solutions
- integrated design
- Replaces 16 separate parts and reduces seal seam length and weight compared to sheet metal designs
- Long runner
- the part related to collision
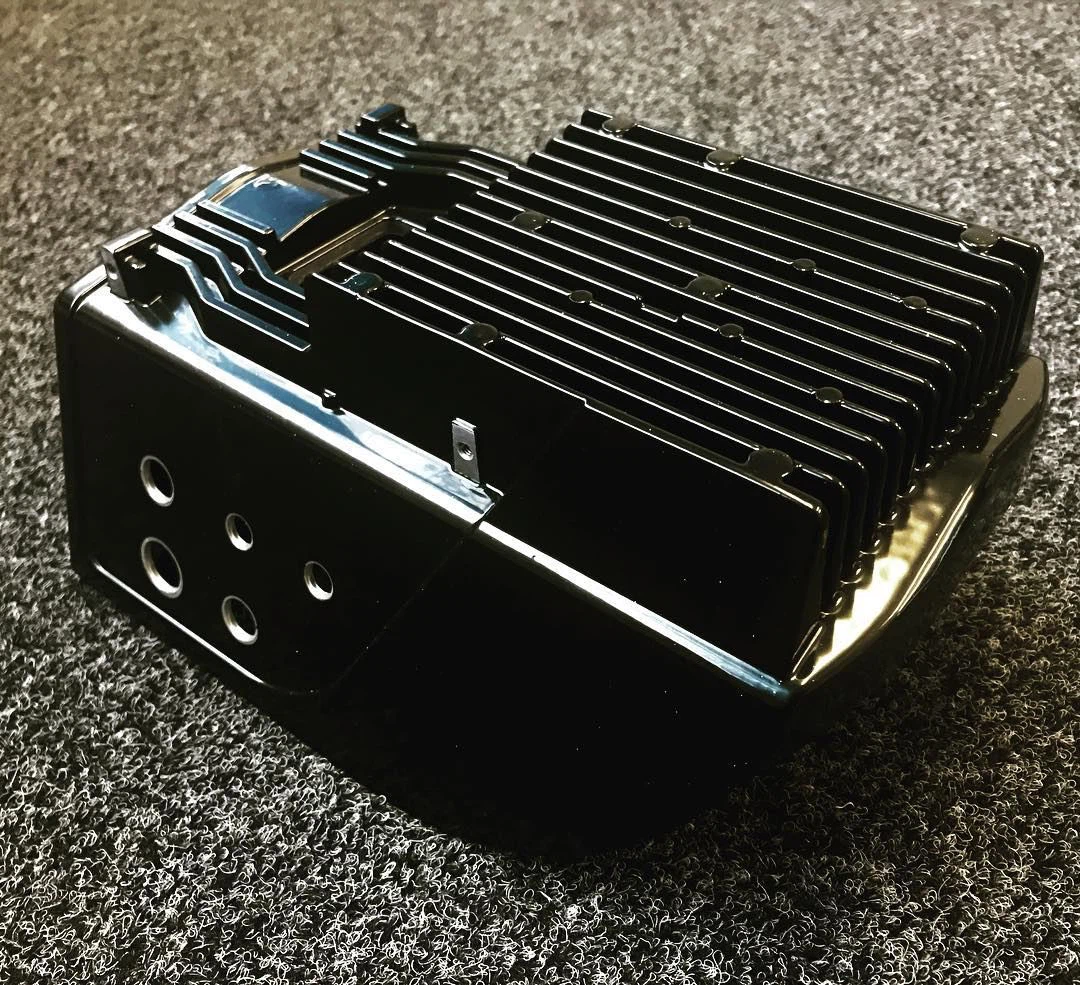
3rd place: 3498 housing with 3D printed samples
Manufacturer: Matteis Die Casting, Germany
Dimensions (LWH): 94 mm x 92 mm x 92 mm
Weight: 450 grams
Alloy: Al Si 12 (230)
Product description: Micromotors for signal acquisition are then installed in four holes located on the 46mm long side. Housings installed later must meet IP56 tightness requirements.
Design, Casting and Forming Requirements: Due to technical requirements, ensure that the large cylinder and inner bore "run out" without errors (see next point for details).
Reason for using the die casting process: In order to ensure that there are no surface or structural defects, the thermal balance of the mold must be optimal, in addition to the pure casting parameters. This is not possible with conventional methods (classical tempering of the core). Casting quality can be improved by using additively manufactured cores in the 3D printing process. In addition, the heat consumption of the mold is reduced and the cycle time is shortened.
Reason for award:
- Classic die casting process combined with innovative additive manufacturing
- Extends the manufacturability limits of traditional die casting processes
- special tempering measures
Appreciation Of The 2022 European Best Magnesium Die Casting Award Winning Magnesium Alloy Die Castings
[Breaking News] Expansion Or Second Factory? Tesla's 1 Million Annual Production Capacity Weighs On Shanghai
Related Article



