
Technical Requirements For The Production Of Die-casting Molds
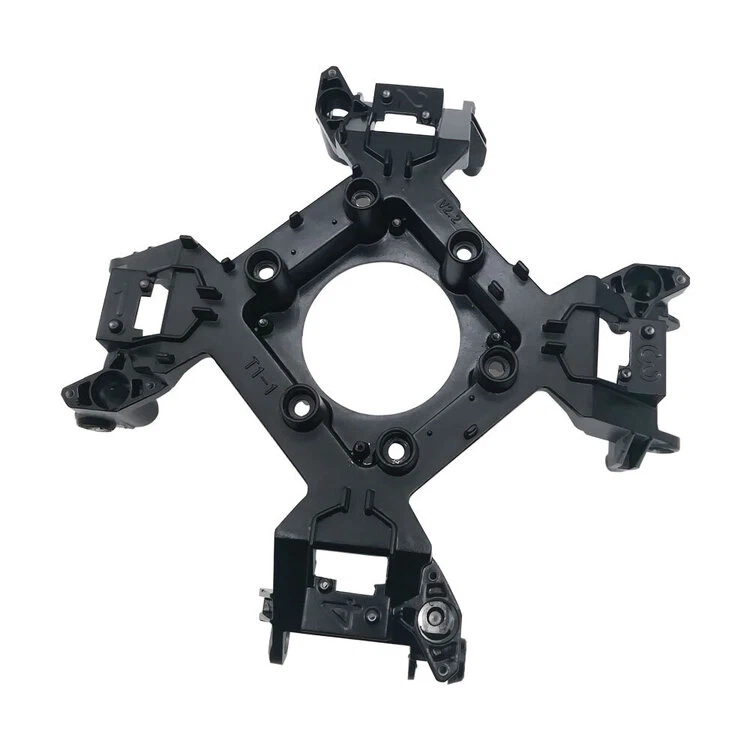
Technical requirements for the production of die-casting molds
The main function of the die-casting mold requires the processing of the plastic film, and the quality of the mold guarantees the quality of the product is self-evident. Different types of plastic products and the molding process of different products have different requirements for the material, function and shape of the mold.
1. With the emergence of high-speed molding machinery, the production speed of plastic products has continued to increase. Since the molding temperature is generally between 160 and 350°C, the fluidity of some parts is not good, and the molding speed is fast, so that the molding surface temperature of the mold parts exceeds 400°C in a very short time. When the working temperature of the mold is high, the hardness and strength of the mold are reduced, leading to early wear or plastic deformation failure of the mold. In order to ensure the accuracy and deformation of the mold during use, the mold steel should have high heat resistance. In order to reduce the temperature rise of die steel, die steel should have good thermal conductivity and low thermal expansion coefficient. 1. For mold blanks smaller than 2020, a mold pit is required between A and B; for mold pits larger than 2020, all templates including thimble plates must be broken.
2. The guide pin and sleeve of the mold should be processed to the exhaust groove to prevent the guide pin and sleeve from being pulled.
3. There must be no sharp corners on the mold, and chamfering is required. Unless otherwise specified.
4. Without consent, the inner mold and mold parts shall not be welded.
5. The periphery of the mold product must be opened in the proper position. Please refer to the mold design manual for the exhaust groove specifications.
6. Try to avoid sanding the mold with a sander. If you need to use a sander, you must use oilstone to save light (especially the parting surface).
7. The surface treatment of the inner mold surface must be carried out in accordance with the technical requirements of the bom table or other official notifications. The processing lines on non-adhesive surfaces (wire cutting, milling machine, CNC trampoline, spark machine) should also be polished with oilstone.
8. All internal mold materials and mold grade requirements must be purchased according to the order, or the technical requirements must be formally confirmed during the design review process. Material certification must be provided, if it is a hard mold, a heat treatment report must be provided. All relevant evidence.
9. All front and back inner molds, inserts, rankings, inclined tops, straight tops (push blocks), shoveling chickens, etc. all need to be processed with a round pit on the bottom or side, and engraved with the material name and hardness.
10. Important wear-resistant parts such as ranking, pushing blocks, shoveling chickens and pouting must be nitrided and hardened.
11. The location must be located. The positioning methods include slingshot, wave beads, Hasco (dimethyl ether) standard positioning clips, etc., which need to meet the requirements of each project. This row needs to have a bead and a wear plate. For hemming and wear-resistant plates, wear-resistant hard materials must be used, and oil grooves are required. . At the working temperature, the working conditions of the molds are mostly very poor, and some often bear relatively large loads, which will cause brittle fracture. The extrusion molding pressure is relatively high, generally 10~35mpa. Therefore, in order to prevent the mold parts from breaking suddenly during use, the mold has high strength and toughness.
12. Wear resistance With the expansion of the use of plastic products, inorganic materials such as glass fibers are often added to plastics to enhance plasticity. Due to the participation of additives, the fluidity of the plastic is greatly reduced, resulting in mold wear. The mold is required to have excellent wear resistance.
Basic Requirements Of Injection Mold
Basic Knowledge And Experience Of Injection Mold
Related Article



