
Domestic Patent: An Extrusion Casting Method For The Metal Mold Of The Main Body Of The Aluminum Alloy Suspension Clamp
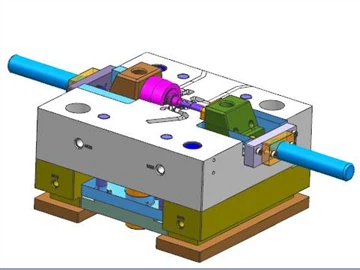
The present invention provides a metal die extrusion casting method for the main body of an aluminum alloy suspension wire clamp. The main body includes an alloy suspension wire clamp. The main material of the alloy suspension wire clamp is ENAC-42100 aluminum alloy. The extrusion casting method includes a smelting stage , Squeeze casting stage and heat treatment.
With the development of my country's electric power industry, transmission line projects are increasing year by year, and there is a huge demand for transmission line fittings. Among the fittings strings of transmission lines, the amount of vertical clamps is the largest, and the corresponding suspension clamps are ordered in large quantities. At present, in transmission lines, suspension clamps made of aluminum alloy are light in weight and have no hysteresis eddy current loss. They are widely used. In recent years, Power operation departments such as the State Grid Corporation have higher and higher requirements for aluminum alloy suspension clamps, and their manufacturing methods have changed from sand mold casting to metal mold gravity casting and low-pressure casting, especially for UHV power transmission projects, which require the use of forging technology Processing suspension clips, and the price should not exceed the upper limit.
Based on the analysis of the above situation, the gravity casting processing method of aluminum alloy suspension wire clamp has the problems of low mechanical properties and heavy weight; the low pressure casting processing method of aluminum alloy suspension wire clamp has the problems of low production efficiency and high production cost; The forging processing method of the suspension wire clip has the problems of many production steps, high energy consumption, low material utilization rate and high production cost. The problems in the above processing methods make the market competition of aluminum alloy suspension clamps more intense. How to develop a processing method with better cost performance, improve the market competition of enterprise products, and save materials and energy is extremely important.
In order to solve the above-mentioned technical problems, the present invention provides a metal mold squeeze casting method for the main body of an aluminum alloy suspension clamp, which relates to the field of suspension clamp manufacturing for power system transmission lines.
The steps in the smelting stage are as follows: preheat the smelting furnace first, make the smelting furnace dry and free of moisture; add ENAC-42100 aluminum alloy, and carry out slag removal at a melting temperature of 745°C; carry out the first argon refining at a melting temperature of 740°C, Each argon refining is preheated argon instead of cold argon; the melting temperature is 745°C for modification treatment, adding trace rare earth elements La and Nd; the melting temperature is 740°C for the second argon refining, standing 15 minutes; the pouring temperature is 690-710 °C, and the pouring is completed within 30 minutes. If the pouring cannot be completed within 30 minutes, continue to carry out argon refining. As time goes on, argon refining can be carried out every 30 minutes;
The steps in the squeeze casting stage are: use a 630T vertical squeeze casting machine to carry out the metal mold squeeze casting process, and install the main mold of the suspension clamp on the vertical squeeze casting machine; pour liquid aluminum alloy at 690-710°C into Inclined deflector; the semi-solid aluminum alloy cooled by the inclined deflector enters the barrel; it is pressed to the metal mold of the main body of the suspension clamp at a ratio of 1 000 kgf/cm2 for the first low-speed filling; at a ratio of 9 00 kgf/cm2 Press to the metal mold of the main body of the suspension clamp for secondary pressure, hold the pressure for 30 s, open the mold and take out the parts;
The heat treatment steps are as follows: the extrusion casting of the main body of the suspension clamp is heated in a furnace, raised to 300 °C, and kept for 30 min; continued to be heated to 400 °C, kept for 30 min; continued to be heated to 500 °C, kept for 1 h; Solid solution temperature (535±5) °C, solid solution for 6 hours; when the temperature is above 535 °C, quickly turn off the fan and open the furnace door, and the product will quickly enter the water with the basket, using dynamic water, shaking the water tank or flowing water, water quenching 10 min, the temperature is about 60 °C; dry the extrusion casting of the main body of the suspension wire clamp; put the dried extrusion casting of the main body of the suspension wire clamp into the aging holding furnace, the aging temperature is 150 °C, and the aging time is 6 h; the main body of the suspension wire clamp is extruded After the die-casting parts are taken out, follow-up surface treatment by shot blasting is carried out.
Compared with the prior art, the present invention has the advantages that the aluminum alloy suspension clamp processed by the metal mold extrusion casting process has better surface quality than the gravity casting suspension clamp compared with the products processed by the metal mold gravity casting process, and saves materials. 40%, good mechanical properties, reaching 300 MPa, close to forged suspension clamps; compared with low-pressure casting process products, the surface quality is better than low-pressure casting suspension clamps, high production efficiency, high process yield; and forging process products In comparison, the production efficiency is high, the production process is less, it belongs to near-net processing, there is no flash burr, no punching die is required, the material utilization rate is high, the surface quality is good, and the comprehensive cost is low. It has excellent mechanical properties, belongs to near net processing, saves materials, high production efficiency, good surface quality, and the overall cost is lower than other aluminum alloy suspension clamp processing methods. It has high cost performance and obvious competitive advantages, and is suitable for vigorous promotion and application.
Disclaimer: This article is originally authorized by the Patent Office to publish the patent. It is for academic exchange only. The data and pictures come from the patent office. If there is any infringement, please contact to delete.
INJECTION MOLD DESIGN Of HIGH-POWER LASER EQUIPMENT BOTTOM CASE + 3D
Five Effective Ways To Improve The Corrosion Resistance Of Magnesium Alloy Materials
Related Article



