
Design and Numerical Simulation of Aluminum Alloy Base Die Casting Process Based on Flow-3D
2023-06-20
The aluminum alloy base is the connecting piece on the filter, and the casting requires a lightweight and complex structure, so it is suitable for production by the die-casting process. Due to the presence of pore defects in the casting, the air tightness of the casting cannot meet the production requirements. Therefore, the design requirements for the die-casting process are relatively high. Flow-3D software can predict the location and amount of entrained air that may occur in the casting. According to the structural characteristics of the aluminum alloy base casting, the die-casting gating system is designed. The numerical analysis of the filling process of the casting process scheme was carried out by using Flow-3D software. According to the obtained temperature field distribution, the distribution and volume of entrained air during the casting-filling process are predicted. According to the simulation results, 8 overflow tanks were set up in places with severe gas entrainment. The simulation results show that the surface temperature difference of the casting is reduced, the entrained gas is basically distributed in the overflow groove, and the filling process is more stable. The actually produced castings have smooth surfaces, fewer internal defects, and improved air tightness.
Graphical results
The dimensions of the aluminum alloy base are 95mm×82mm×80mm. The base is 72mm long and 12mm high, and there are two cylinders with an outer diameter of φ23.2mm and an inner diameter of φ14mm in the middle. The maximum outer diameter of the tapered back flange is φ72mm, and the inner diameter is φ60mm. The three-dimensional model of the casting is shown in Figure 1. The average wall thickness of the castings is 7mm, and the weight of each casting is about 553g. The castings are required to have good airtightness and smooth surfaces. The die-casting machine model selected is DM300. The base material of the aluminum alloy filter is ADC12, and its chemical composition is shown in Table 1.
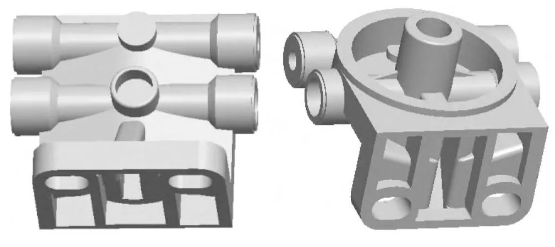
Fig.1 3D model of casting
Table 1 Chemical composition of ADC12 alloy (%)
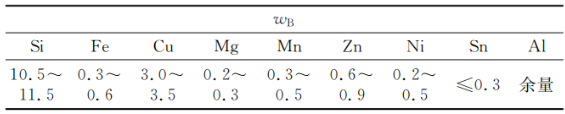
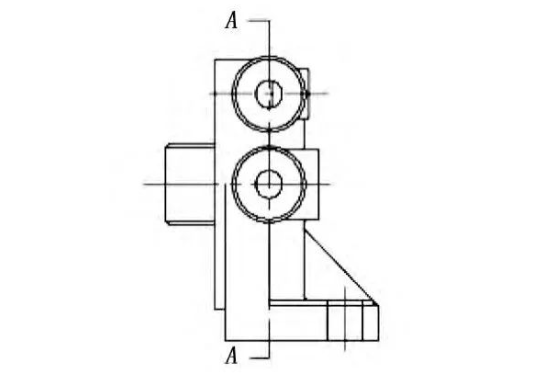
Figure 2 Parting surface of the casting
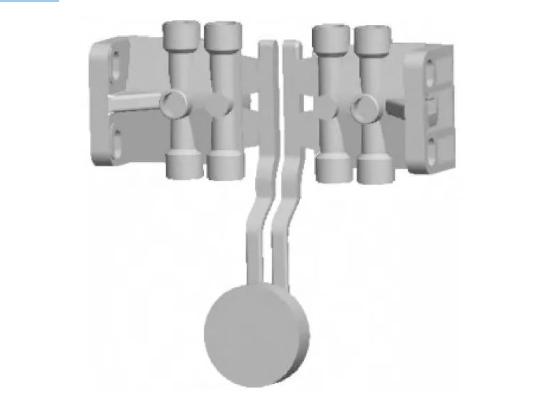
Figure 3 Casting with gating system
The mold-filling process is simulated according to the designed gating system, and the VOF algorithm in the Flow-3D software is used, that is, the free fluid surface tracking method. During the calculation, when the fluid elements split or gather, the fluid surface automatically appears, merges, or disappears, and the high-speed flow state of the liquid can be accurately observed. First, save the casting model with the gating system in STL format in Pro/E software, and import it into Flow-3D simulation software. Set the die-casting parameters: the pouring temperature is 680°C, the mold temperature is 230°C, the mold material is H13, and the gate speed is 30m/s; in the physical model options of the Flow-3D software, select entrainment, surface defect tracking, gravity, and heat transfer, viscosity model, etc.
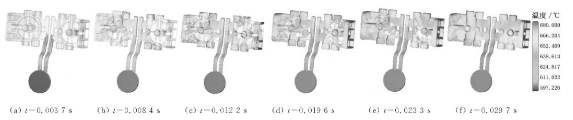
Figure 4 Casting filling process with gating system
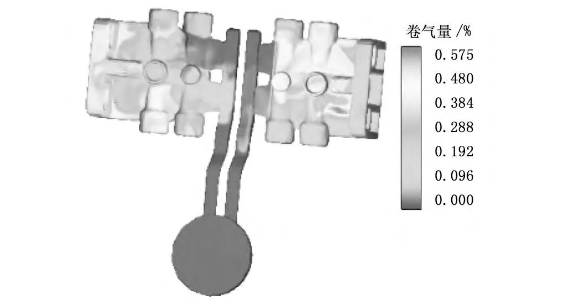
Fig. 5 Entrained gas distribution of castings with gating system
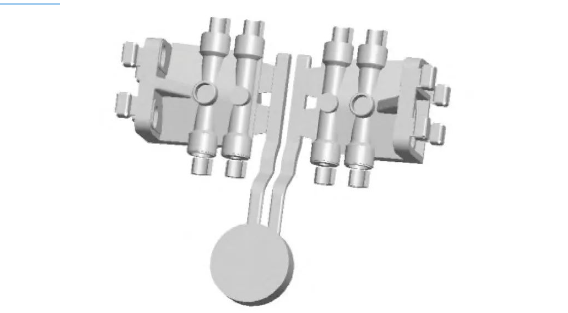
Fig.6 3D view of casting with gating system and overflow groove
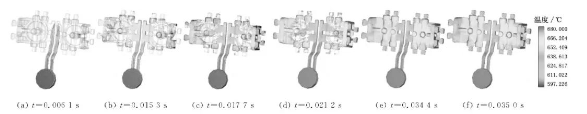
Fig. 7 Filling process of casting with gating system and overflow groove
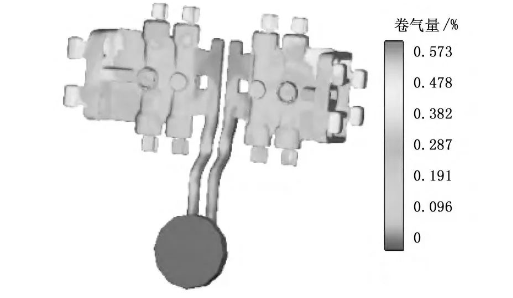
Fig. 8 Entrained air distribution of casting with gating system and overflow groove
Figure 9 Actual production of castings
A reasonable gating system was designed according to the structural characteristics of the casting, the filling process was simulated by Flow-3D software, and a reasonable overflow groove was designed by analyzing the simulation results. The simulation results again show that the setting of the overflow groove obviously reduces the defects such as pores of the casting. The actual castings produced meet the leak detection standard, which improves the quality of the castings and reduces the production cost.
What material is 5% as dense as steel but 10 times stronger?
The Benefits of Die Casting Technology in Manufacturing
Related Article

Fast sampling is the fastest way to win business in the hardware machining and plastic mold industries. Customers want a working sample in days, and a 3D printer delivers it, but only when you know how to print in 3d correctly.
how to print in 3d

Fast sampling is the fastest way to win business in the hardware machining and plastic mold industries. Customers often send an STL file and expect a working sample in days.
how to print an stl file

