
Basic Knowledge And Experience Of Injection Mold
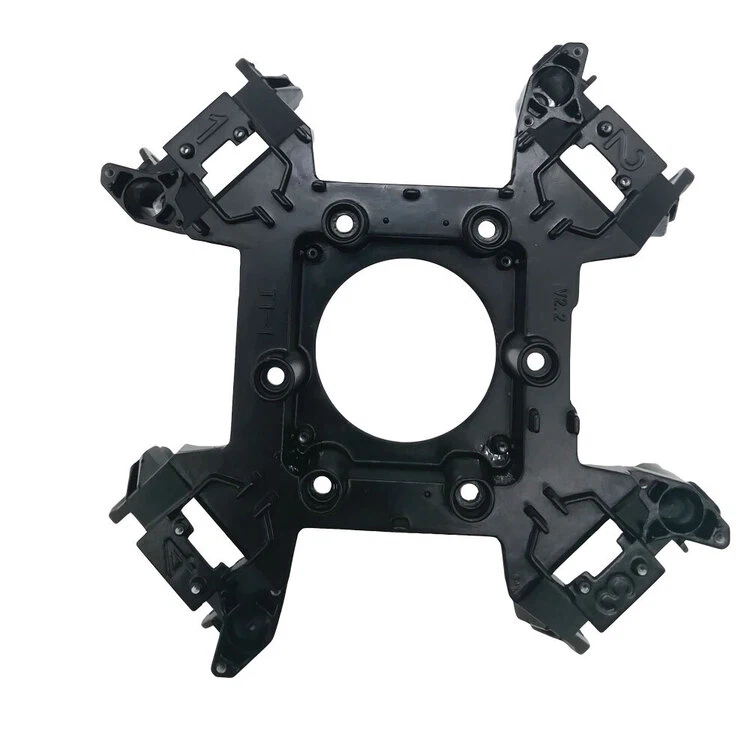
Basic knowledge and experience of injection mold
The basic knowledge of the mold is to tell the basic composition of the mold, the influence of the shape on the product, and the introduction of the mold model.
1. The basic composition of the mold
(1) Front mold (main mold) (fixed mold), (2) rear mold (outer mold) (moving mold), (3) insert (inlay), (4) rank (slider), (5) ) Inclined top, (6) thimble, (7) gate (water inlet)
2. The influence of mold product shape on product
Wall thickness, geometry, will affect forming shrinkage, draft angle
three. The influence of water inflow on product shrinkage
When the size of the water inlet is larger, the shrinkage rate is smaller; when the size of the water inlet is smaller, the shrinkage rate is larger, the water flow direction is parallel, the shrinkage rate is larger, and the vertical direction is smaller.
Some people say that after I analyze the product structure, I can start designing the mold. The answer is of course no. If you want to avoid detours in the design process, some items that affect the mold structure must be confirmed. The specific content is as follows: 1. The tonnage and model of the injection molding machine used by the customer. This confirmation is not good. Unable to determine the entrance diameter of the mold sprue bushing and the diameter of the positioning ring. The position, and the depth of the injection molding machine into the mold, even the size of the mold base, the closing height, and so on. You have worked hard to design a mold structure with a cylindrical core. You also have a sense of accomplishment. The mold cannot be produced by the customer. Because the customer only has an electric injection molding machine and there are no extra neutrons, it is estimated that you will feel crying. 2. The coding method of the customer's injection molding machine, commonly used include platen coding mold, screw coding method, hydraulic coding method, magnetic coding method, etc. This confirmation is good, you know that you do not need to design the pattern screw hole or code slot, design the mold. 3. The problem points of the product we just analyzed, as well as product clamping, product material and shrinkage rate. Don't take it for granted that the shrinkage rate of pp plastics must be 1.5%. This must be confirmed with the customer to understand their final production grade, whether to add any modified materials, etc.
(1) In order to ensure the strength and rigidity of the product without making the wall thickness of the plastic part thinner, reinforcing ribs can be set at the appropriate part of the plastic part to prevent deformation. In some cases, it can improve the plastic flow problem during the forming process.
(2) The thickness of the ribs should not exceed 50% of the plastic parts, generally around 20%.
(3) The rib should be lower than the plane of the plastic part
Technical Requirements For The Production Of Die-casting Molds
Process Flow Of Injection Mold
Related Article



