
How Are Gears Manufactured? A Step-by-Step Guide to Gear Production
Author: SZTC
2025-04-19
Gears are essential mechanical components that transmit power and motion in countless applications, from automotive transmissions to industrial machinery. Their precise design and manufacturing are critical to ensuring smooth operation and durability. In this blog, we’ll explore the primary methods and step-by-step processes involved in gear manufacturing, covering traditional techniques and modern advancements.

Core Manufacturing Methods for Gears
Cutting (Machining)
Cutting is the most common method for producing gears, suitable for both low-volume and high-precision applications. It involves using specialized tools to remove material from a blank (usually a cylindrical workpiece) to form gear teeth. Key cutting techniques include:
- Hobbing: A hobbing machine uses a spiral-shaped hob (a cutting tool) that mimics the shape of the gear teeth. The hob rotates and feeds into the blank, creating teeth through a continuous cutting motion. This method is highly efficient for producing spur, helical, and worm gears.
- Shaping: A gear shaper uses a reciprocating cutting tool (shaper cutter) that moves vertically while the blank rotates in sync. This is ideal for internal gears or gears with complex geometries that are hard to machine with hobbing.
- Broaching: Used for producing internal gears (e.g., splines), a broach tool with progressively sized teeth is pulled or pushed through the workpiece to create the gear profile.
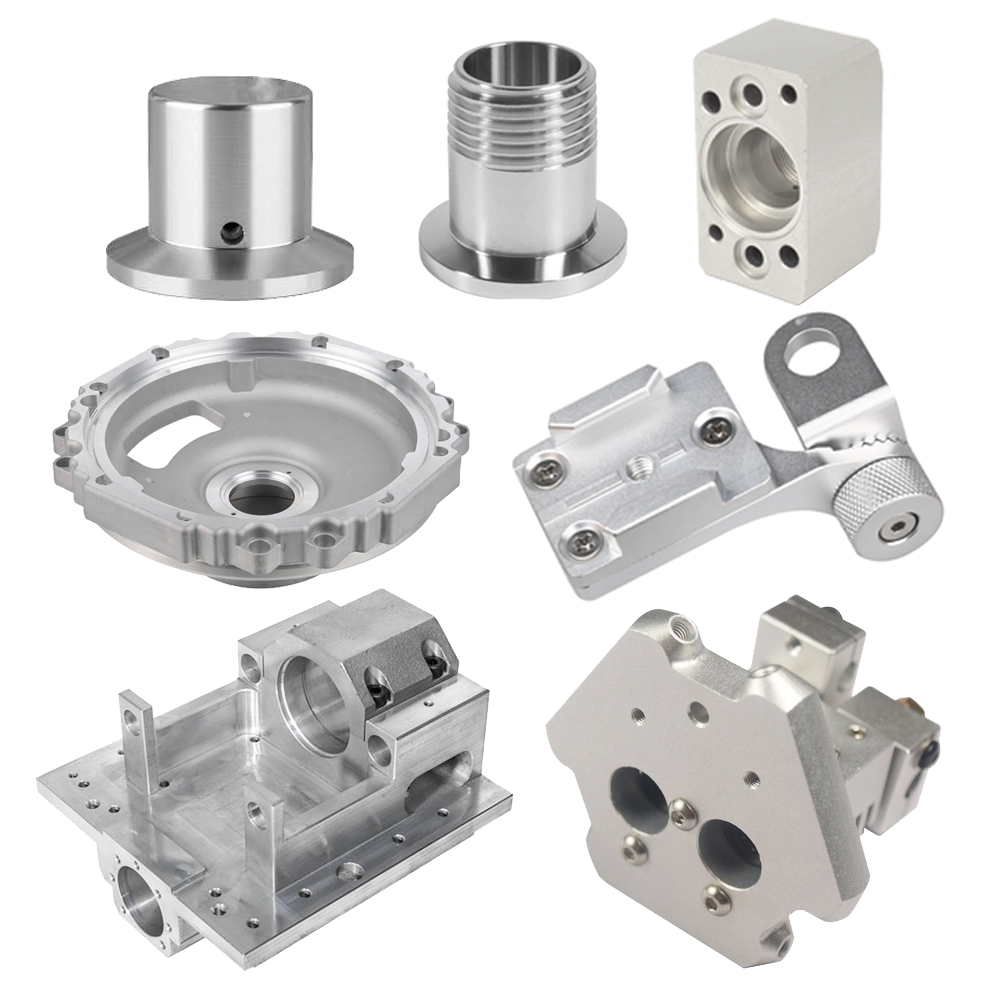
Forming involves shaping the gear teeth by deforming the material rather than cutting it, making it suitable for high-volume production. Two main forming methods are:
- Rolling (Gear Hobbing vs. Gear Rolling): In gear rolling, a hardened steel roller with the inverse tooth profile presses into the heated blank, plastic-deforming the material to create teeth. This method offers high efficiency and good surface finish, often used for gears in automotive transmissions.
- Casting: Metal casting (e.g., sand casting or investment casting) can produce gears by pouring molten metal into a mold with the desired tooth shape. While less precise than cutting, casting is cost-effective for low-stress applications like agricultural machinery.
Grinding and Finishing
After cutting or forming, gears often undergo finishing processes to improve accuracy and surface quality:
- Gear Grinding: A grinding wheel with the shape of the gear tooth flank is used to refine the tooth profile, removing heat treatment distortions and achieving high precision. This is critical for gears in aerospace or high-speed applications.
- Lapping and Honing: These processes use abrasive materials to smooth the tooth surfaces, reduce friction, and improve noise reduction. Lapping involves rubbing the gear against an abrasive-coated lap, while honing uses a rotating abrasive tool.
Step-by-Step Gear Manufacturing Process
1. Material Selection
Gears are typically made from metals like carbon steel, alloy steel (e.g., chromium-nickel steel for strength), or non-ferrous materials (e.g., brass for low-load applications). Plastics (e.g., nylon) are used for quiet, low-power gears in appliances. The material must withstand wear, fatigue, and the specific mechanical loads of the application.
2. Blank Preparation
The raw material is shaped into a blank, usually a cylindrical piece, through processes like forging (to improve grain structure and strength) or machining from a bar stock. The blank’s dimensions are slightly larger than the final gear to allow for material removal during cutting.
3. Gear Cutting/Forming
Depending on the method:
- Hobbing: The blank is mounted on a hobbing machine, and the hob cuts the teeth in a helical or straight pattern, guided by the machine’s precision controls.
- Rolling: The blank is heated to enhance ductility, and the rolling tool stamps the tooth profile into the material in a single pass or multiple stages.
4. Heat Treatment
Heat treatment processes like carburizing (adding carbon to the surface), quenching (rapid cooling), and tempering (reheating to reduce brittleness) are used to:
- Increase surface hardness for wear resistance.
- Maintain core toughness to prevent fracture under load.
- Example: A carburized gear may have a surface hardness of 60 HRC (Rockwell hardness) while the core remains softer (30-40 HRC).
5. Finishing Operations
- Deburring: Removing sharp edges or burrs from the teeth to ensure smooth operation.
- Grinding/Honing: As mentioned earlier, to achieve tight tolerances (e.g., ISO gear accuracy grades 4-6 for precision applications).
- Surface Coating: Applying treatments like shot peening (to improve fatigue strength) or plating (e.g., nickel-phosphorus for corrosion resistance).
6. Quality Inspection
Gears are inspected for dimensional accuracy (tooth profile, pitch, backlash), surface finish, and mechanical properties using tools like:
- Coordinate Measuring Machines (CMMs) for precise geometry checks.
- Gear testers to measure tooth contact pattern and noise during rotation.
- Magnetic Particle Inspection (MPI) or Ultrasonic Testing to detect internal defects.

Modern Advancements in Gear Manufacturing
CNC Machining and Automation
Computer Numerical Control (CNC) technology has revolutionized gear production by enabling highly precise, automated cutting and grinding. CNC hobbing machines, for example, use computer programs to control the hob’s movement and the blank’s rotation, ensuring consistent tooth spacing and profile accuracy. Automation reduces human error and allows for mass production of complex gears like bevel or worm gears.
Additive Manufacturing (3D Printing)
While traditional methods dominate, 3D printing is emerging for specialized gears. Processes like selective laser melting (SLM) with metal powders or fused deposition modeling (FDM) with polymers can create intricate gear geometries that are difficult to machine, such as internal gears with undercuts or hybrid gear systems. Additive manufacturing is ideal for prototyping, low-volume production, or gears with customized tooth profiles.
Gear Skiving
Skiving is a newer machining technique that combines elements of hobbing and shaping. It uses a rotating skiving tool to cut gears, offering advantages in producing gears with small diameters, high aspect ratios, or in hard-to-reach spaces (e.g., near shoulders or flanges). Skiving is particularly useful for automotive gears and aerospace components.
Simulation and Digital Twin Technology
Advanced software simulations (e.g., finite element analysis, FEA) allow engineers to predict gear performance under various loads, optimize tooth profiles, and reduce material waste. Digital twin technology creates virtual replicas of the manufacturing process, enabling real-time monitoring and adjustments to ensure consistent quality and efficiency.

Conclusion
Gear manufacturing is a blend of precision engineering, material science, and technological innovation. Whether using traditional cutting methods, modern CNC automation, or emerging additive techniques, each step—from material selection to heat treatment and inspection—is critical to producing gears that meet the rigorous demands of their applications. As industries evolve toward smarter, more efficient manufacturing, gear production will continue to adapt, leveraging new technologies to create stronger, quieter, and more reliable mechanical systems.
How to Remove Rust from Stainless Steel: Effective Methods and Prevention Tips
What is Zamak? A Comprehensive Guide to the Versatile Zinc Alloy
Related Article

Fast sampling is the fastest way to win business in the hardware machining and plastic mold industries. Customers want a working sample in days, and a 3D printer delivers it, but only when you know how to print in 3d correctly.
how to print in 3d

Fast sampling is the fastest way to win business in the hardware machining and plastic mold industries. Customers often send an STL file and expect a working sample in days.
how to print an stl file

