Does porsche ag manufacture cars requiring cnc machined parts?
Does Porsche AG Manufacture Cars Requiring CNC Machined Parts? A Practical Guide to Custom Precision CNC Machining for High-Performance Automotive Buyers
Most automotive sourcing engineers do not lose sleep over the theory of Does Porsche AG Manufacture Cars Requiring CNC Machined Parts. They lose sleep over the practical version: can this supplier hold the tight tolerance for Porsche-grade automotive components, will the material certificate match what I paid for, will the first article pass incoming inspection, and will the parts arrive before the vehicle prototype or assembly line starts. That is the real reason people search Does Porsche AG Manufacture Cars Requiring CNC Machined Parts at eleven at night with a STEP file open on a second screen.
This guide is written for procurement engineers and sourcing teams who need to evaluate a machining partner for premium automotive performance parts rather than read a textbook. It covers whether Porsche relies on CNC components, the machining types used for Porsche vehicles, the parameters our factory works to, the automotive applications they serve, and a selection checklist you can reuse on every RFQ for performance auto parts. Every number in the specification section is traceable, because a supplier that cannot document its capability should not be quoting your automotive project.
- Does Porsche AG Use CNC Machined Parts?
- Common CNC Machining Types for Porsche Automotive Parts
- Technical Parameters and Data Sources
- Porsche Automotive Applications of CNC Machined Parts
- How to Select an Automotive CNC Machining Supplier: 8 Steps
- FAQ: Porsche-Grade CNC Machining Parameters and Capabilities
- Conclusion and Quote Request
Does Porsche AG Use CNC Machined Parts?
Yes, Porsche AG manufactures sports cars, GT racing models, classic restoration vehicles and electric performance vehicles that heavily rely on CNC machined components. CNC subtractive manufacturing removes material from solid billet, forged or cast blanks to produce finished engine, suspension, chassis and drivetrain parts. A CAD model becomes a toolpath in CAM software, the toolpath is post-processed into G-code, and the machine executes it with servo-driven axes and a controlled spindle.
The practical consequence is simple: the geometry lives in the file, not in the operator's hands. Repeat orders twenty months later still match the first shipment, and any deviation appears as a number in a dimensional report rather than an argument. That repeatability is why automotive precision CNC machining became the default route for Porsche critical functional metal and engineering plastic parts.
A typical Porsche-style automotive job runs through six stages: DFM review for automotive requirements, CAM programming and simulation, fixture setup with first-article measurement, production with in-process checks, deburring and automotive-grade surface treatment, then final inspection and packing. A competent supplier flags features that cannot be cut or inspected during quotation, not after the first article fails automotive incoming QC.
What CNC machining is not matters just as much. It is not injection molding, so there is no tooling amortization and no penalty for a low quantity of classic Porsche spare parts or prototype racing components. It is not 3D printing, so you get full-density material with isotropic properties instead of layer-dependent strength. It sits between hand-fabrication and die-based mass production: the right route for performance prototypes, racing fixtures, custom chassis components and any part where tight tolerance drives the decision more than unit piece price.
Our factory runs one-stop custom automotive CNC machining, not catalogue sales. We do not stock standard off-the-shelf auto parts and we do not resell. Every component is produced from your drawing or 3D model, in the material and finish you specify, inspected to the automotive tolerance you call out, and documented with the reports your quality department will ask for. If you need a standard stock fastener, we will say so and point you elsewhere; if you need a machined suspension bracket with a 0.005 mm bore position for performance vehicles, that is our job.
Common CNC Machining Types for Porsche Automotive Parts
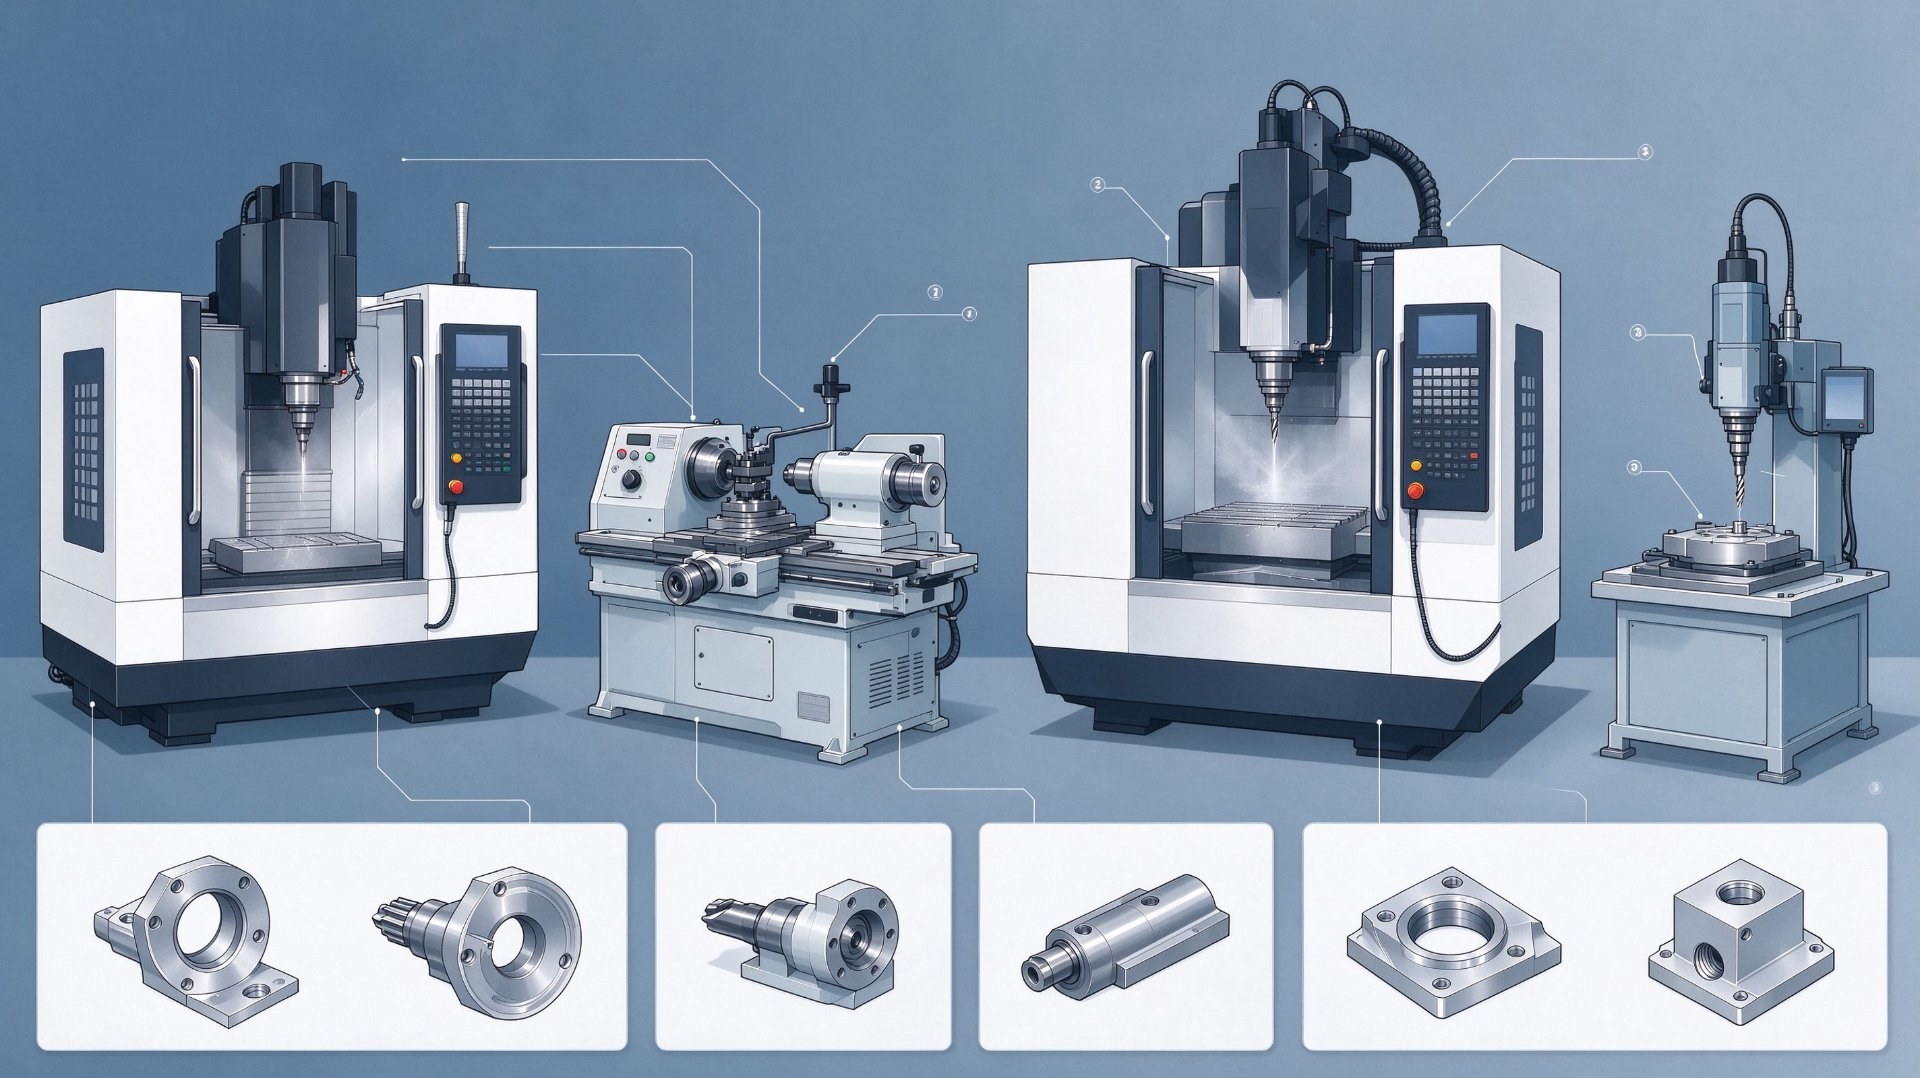 The phrase covers a family of processes. Choosing the wrong one adds cost without adding value, so it helps to know what each is good at for high-performance automotive work.
3-axis CNC milling moves the tool in X, Y and Z against a fixed workpiece. It handles prismatic housings, mounting plates, simple brackets and pockets reachable from one direction, usually in up to three setups for the remaining faces. It is the most economical option for non-critical automotive fixtures and covers whenever geometry allows it.
4-axis CNC milling adds rotation about one axis, usually a rotary table or indexer. It eliminates re-fixturing for parts with features on four sides, such as manifold blocks, valve housings and connector housings, and improves position accuracy between faces because features are cut in one coordinate system instead of being stacked across setups.
5-axis CNC machining adds two rotational axes, letting the tool approach from nearly any direction. This is widely used for Porsche engine parts, complex suspension components, impeller-style cooling parts and contoured racing components. It allows shorter, stiffer tooling that improves surface finish in deep cavities and protects critical datum relationships in a single setup.
CNC turning rotates the workpiece against a stationary or driven tool. Shafts, bushings, spacers, pins, fittings and threaded fasteners for drivetrains belong here, and turning delivers excellent roundness and concentricity when the part is gripped properly. Turn-mill centres combine both operations in one machine for parts that would otherwise need two suppliers, such as valve bodies with cross-drilled oil ports.
Drilling, tapping, boring and reaming usually ride along with milling or turning, yet hole quality decides whether the engine or suspension assembly goes together. Position tolerance, roundness, thread class and depth must be specified rather than assumed, and boring or reaming delivers the straightness and low roughness required for bearing seats and hydraulic bores in performance vehicles.
Surface grinding and lapping remain the route to the flattest, finest surfaces: when a drawing calls for Ra 0.4 μm or parallelism under 0.005 mm on a hardened automotive part, grinding belongs in the process chain. Wire EDM and laser cutting should sit in the same supply chain, because a hardened slot for racing linkage should not be split across three vendors with three separate tolerance standards.
Technical Parameters and Data Sources
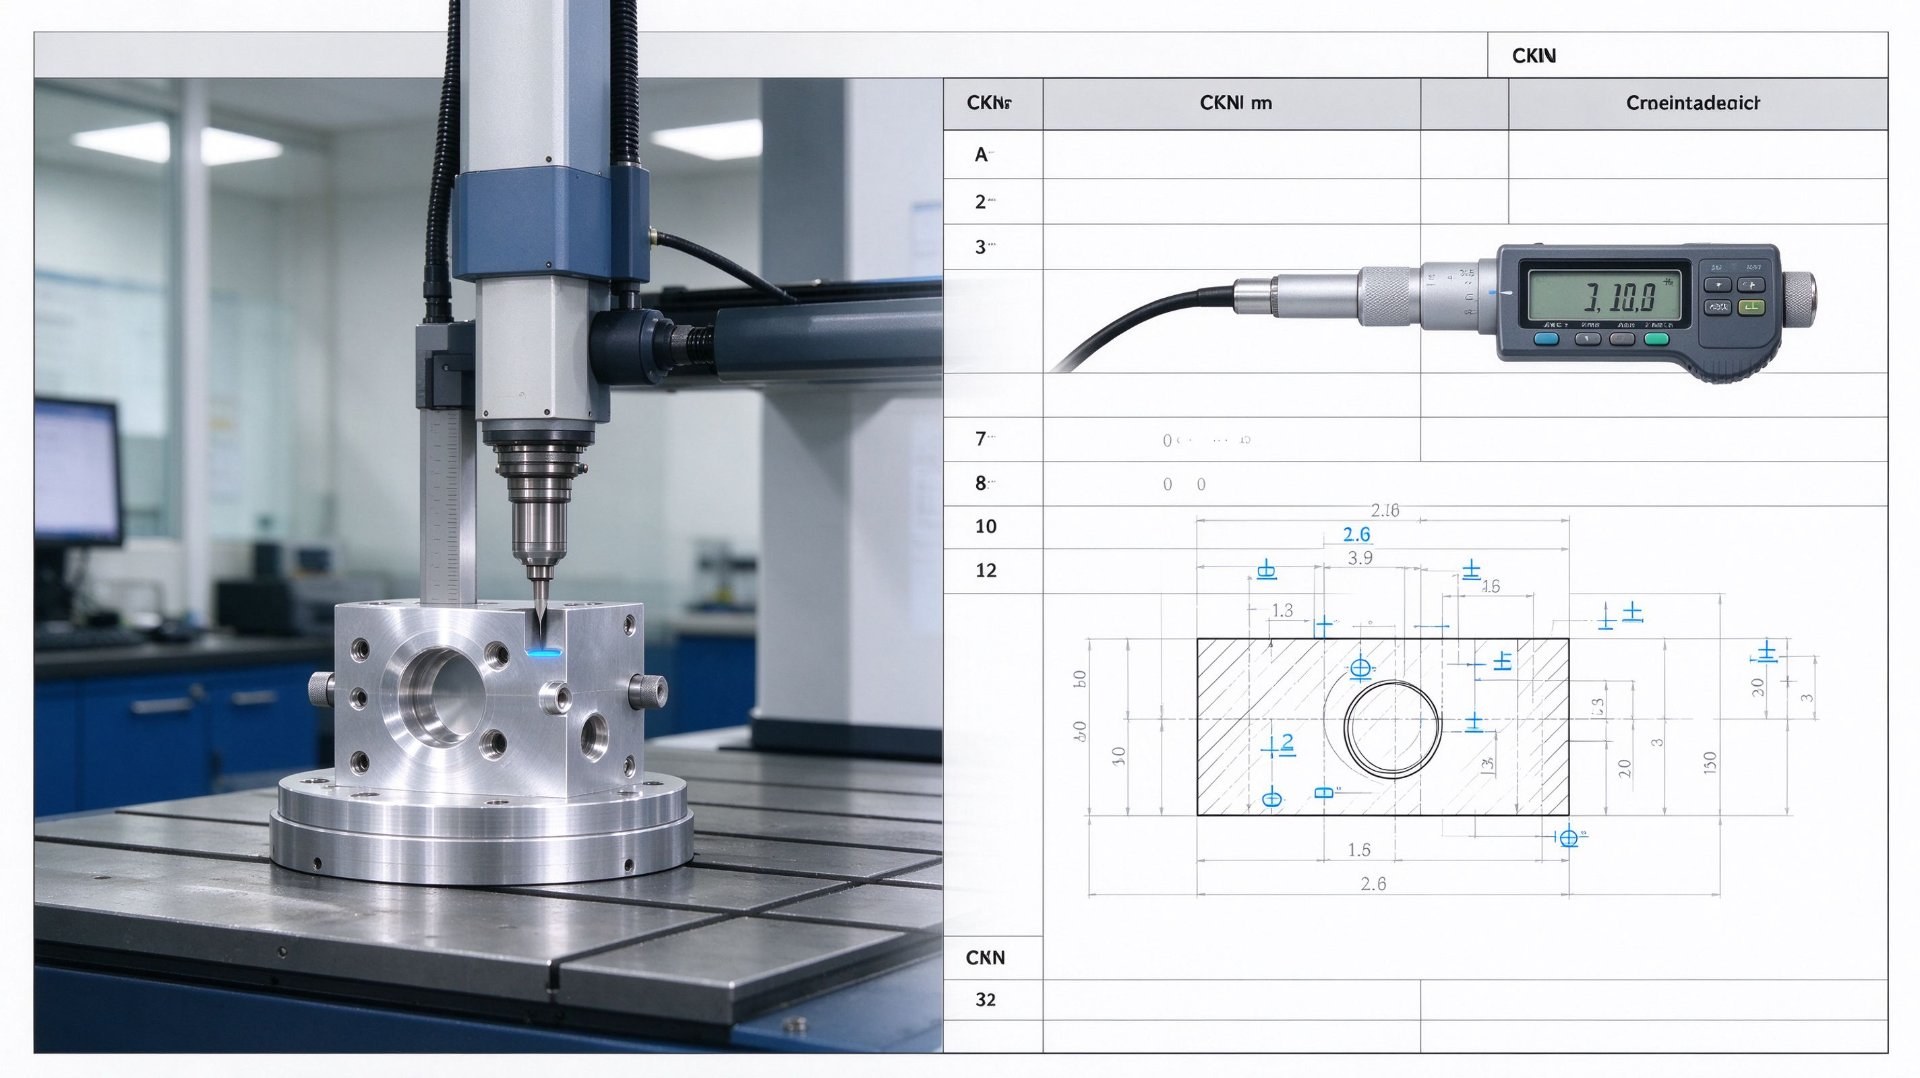 The table states the capability bands our production floor quotes against for Porsche-style automotive precision parts. Any number outside these bands needs an engineering review before we commit, because promising a tolerance a process cannot hold is the fastest way to fail a first article inspection for automotive projects.
| Parameter | Capability | Typical Automotive / Porsche Use |
|---|---|---|
| General tolerance | ±0.02 mm | Mounting brackets, covers, secondary mechanical parts |
| High precision tolerance | ±0.005 mm | Bearing seats, engine mating bores, suspension datum features |
| Surface roughness | Ra 6.3 μm as-machined, Ra 1.6 μm standard, Ra 0.8 μm fine, Ra 0.4 μm by grinding or lapping | Sealing faces, sliding surfaces, engine contact surfaces |
| Milling envelope | Up to 1200 × 800 × 500 mm | Large engine housings, chassis plates, fixture bases |
| Turning envelope | Up to Ø400 × 1000 mm | Shafts, sleeves, wheel hubs, flanges |
| Minimum order quantity | 1 piece prototype, no tooling charge | Racing samples, classic spare parts, engineering validation builds |
| Lead time | 5–7 working days for prototypes, 12–18 working days for 100–1000 pieces | Prototype development, restoration project scheduling |
| Drawing formats | STEP, IGES, X_T, DWG, DXF, PDF | Quotation and 5-axis programming input |
| Tolerance standard | ISO 2768-m / ISO 2768-f, GD&T per ASME Y14.5-2018 | Untoleranced dimensions and automotive inspection disputes |
| Quality system | ISO 9001:2015 aligned process control, FAI report, material certificate, dimensional report | Automotive supplier qualification and incoming inspection |
Material coverage. Aluminum 6061-T6, 7075-T6 and 2024 for lightweight suspension and housing components; magnesium alloy for lightweight crankcases; titanium for racing fasteners and high-temperature parts; stainless 303, 304, 316L and 17-4PH for corrosion-resistant drivetrain hardware; brass C360 and copper C110 for sensor and electrical fittings; carbon steel 1045, 4140 and 4340 for high-strength load-bearing parts; and engineering plastics including POM, PEEK, PTFE, PA6 for insulation and chemical resistance.
Surface treatment and inspection. Anodizing Type II and Type III hard anodize, sandblasting, passivation, zinc and nickel plating, powder coating, laser marking and polishing, each specified with a standard and colour reference, because "black anodized" alone is not a purchasing specification for automotive performance parts. Inspection uses a CMM for positional and form verification, a vision system for small features, a roughness tester, a hardness tester, height gauges and thread gauges.
Data sources: capability bands come from our internal process capability list and inspection standard, November 2026; general tolerances follow ISO 2768-1:1989 and ISO 2768-2:1989; geometric tolerancing follows ASME Y14.5-2018; quality control follows an ISO 9001:2015 aligned system.
Porsche Automotive Applications of CNC Machined Parts
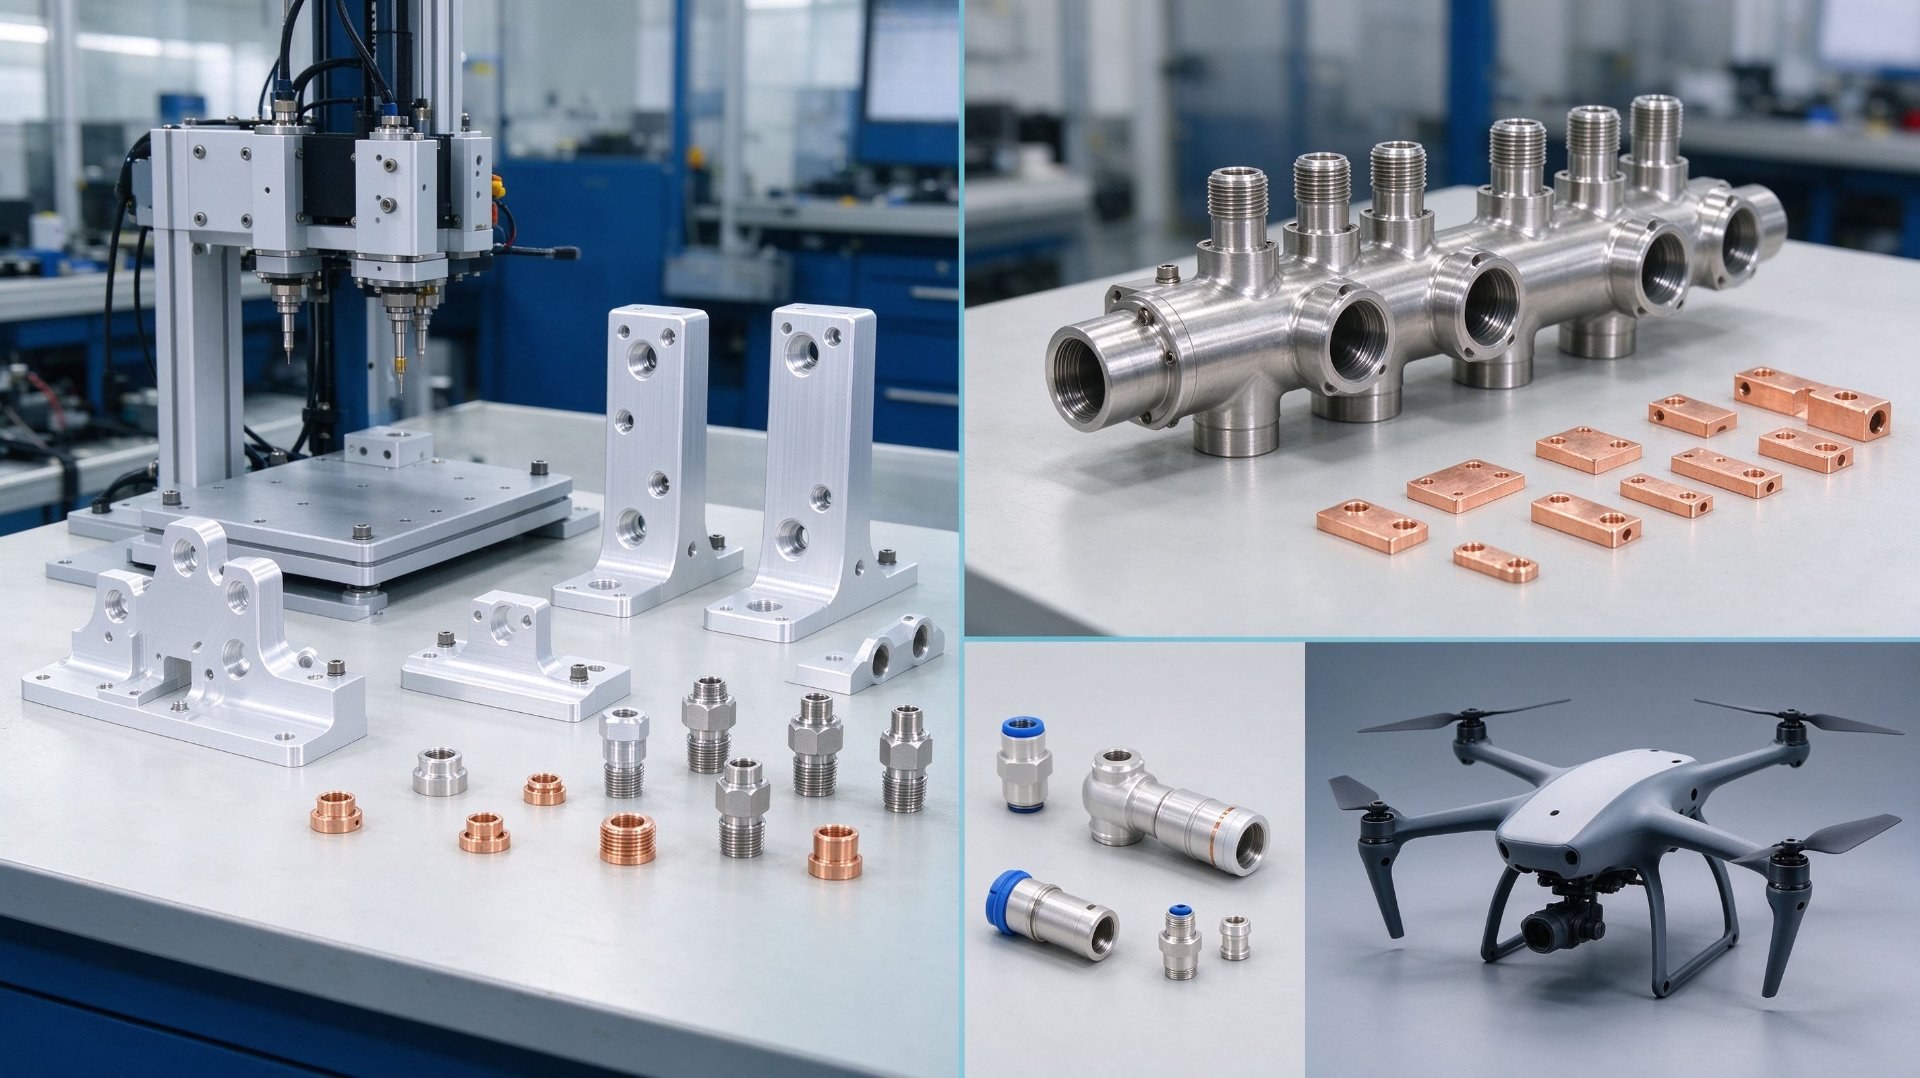
Custom machined parts for Porsche-style vehicles cover these core areas, and each one stresses a different machining capability.
Engine and drivetrain components. Crankcase finishing, cylinder heads, valve housings, bearing caps, piston carriers, shift forks and gear housing sections. Datum control and sealing surface flatness are critical, and material heat resistance and fatigue strength are mandatory for high-rev sports engines.
Suspension, steering and chassis. CNC billet aluminum control arms, steering brackets, wheel hubs, subframe mounts and adjustable racing linkage parts. Thin-wall billet parts require careful fixturing to avoid deflection during 5-axis machining.
Classic Porsche restoration spare parts. Obsolete discontinued original parts reproduced by CNC machining for Porsche Classic projects. Low-volume runs are economically viable without expensive casting molds, and parts follow original drawing dimensions and tolerances.
Racing and GT prototype parts. Aerodynamic fixture mounts, test jigs, cooling system manifolds, lightweight brackets and custom drivetrain hardware for Weissach R&D validation. Fast sample turnaround is critical for iterative prototype testing.
Hydraulic and pneumatic systems. Valve bodies, manifold blocks, pistons, rod ends and port fittings for brake and clutch systems. Bore roundness, straightness, thread quality and sealing-face finish decide whether the assembly leaks, and cross-drilled passages make 4-axis and 5-axis capability a hard requirement.
Instrumentation and sensor mounts. Custom sensor brackets, gimbal mounts and housing blocks for onboard telemetry, camera and pressure sensing systems on performance and race vehicles.
How to Select an Automotive CNC Machining Supplier: 8 Steps
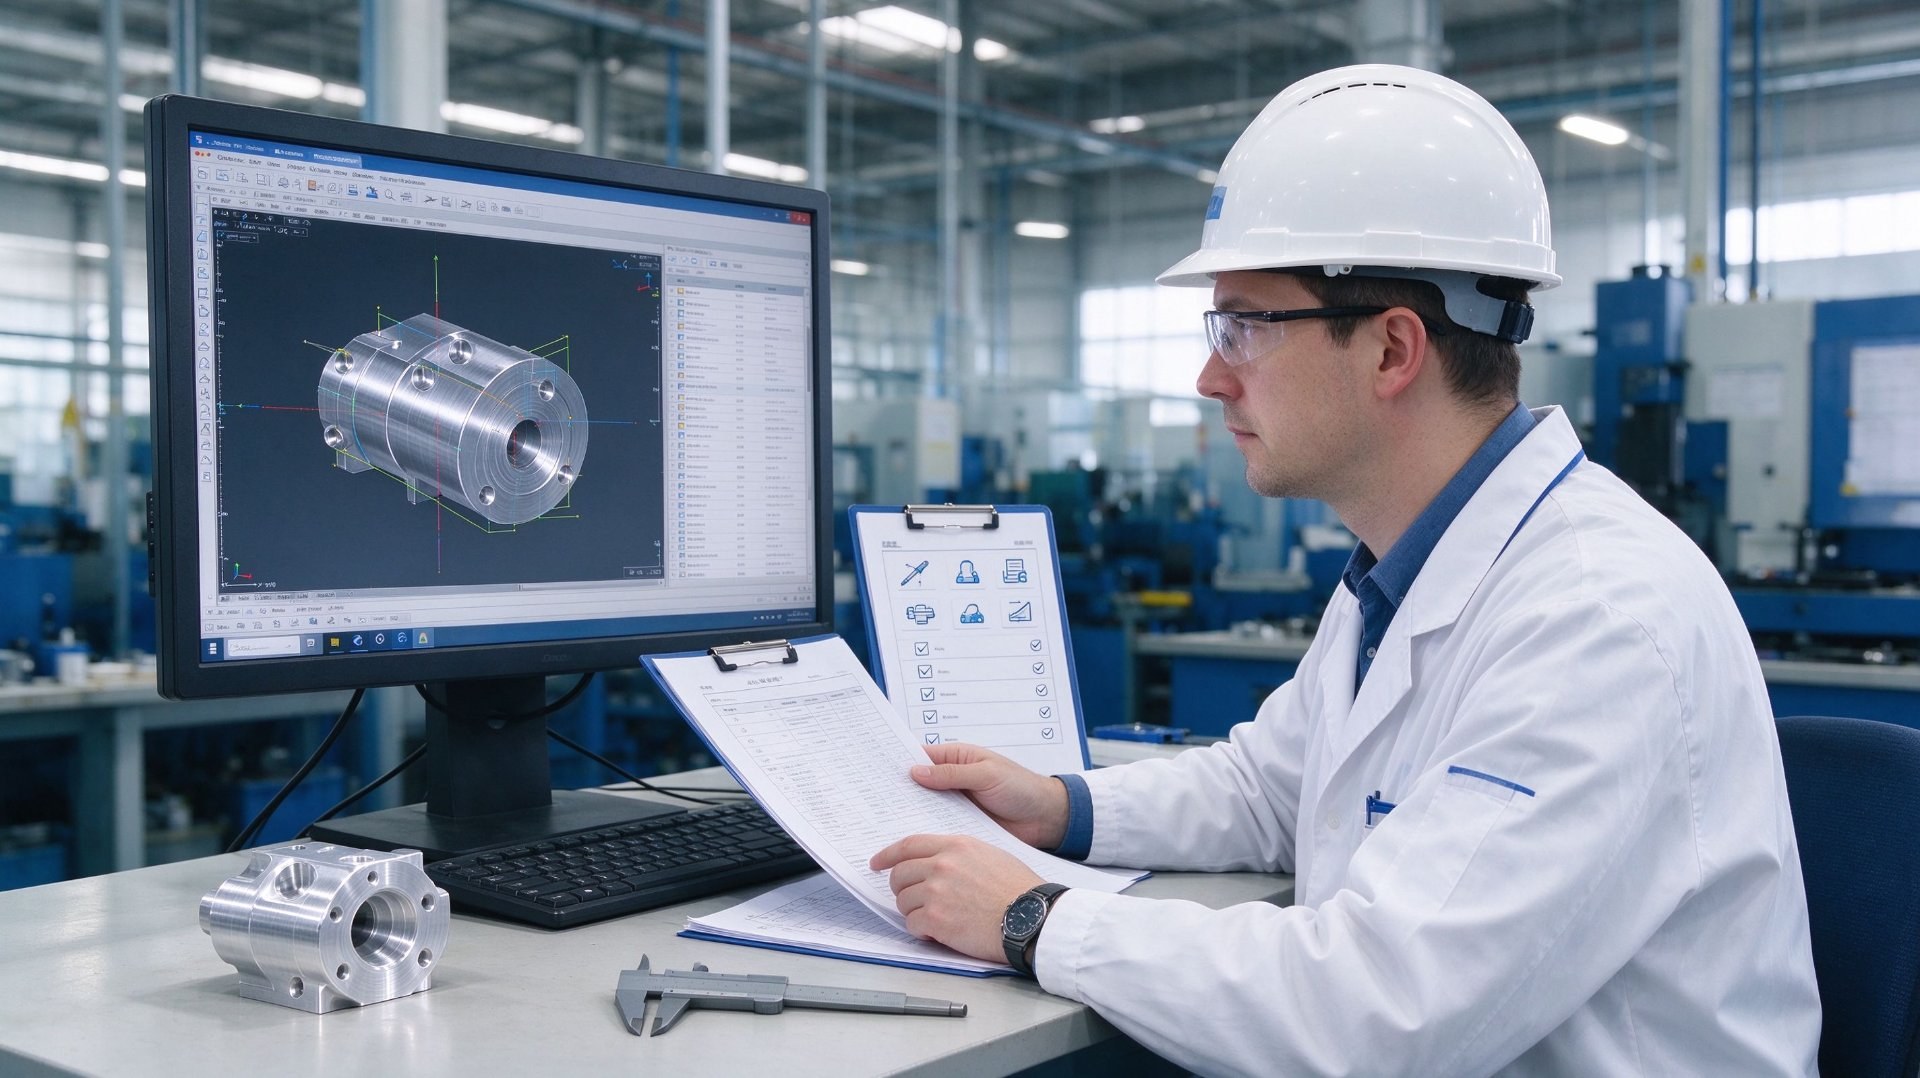
Most automotive sourcing failures are predictable and can be avoided before the purchase order is issued. This sequence is the one we recommend to buyers evaluating us and to buyers evaluating anyone else for performance automotive parts.
Step 1: Send a complete data package. A STEP or X_T model for geometry and a 2D drawing for tolerances, datums, threads, finish, material, heat treatment and marking. A model alone leaves critical dimensions to interpretation, and interpretation is where disputes start. State quantity, target date, destination country and packaging requirement.
Step 2: Ask for DFM feedback before price. A serious supplier comments on wall thickness, tool reach, corner radii, tolerance stack-up and whether your finish is achievable on the automotive geometry you drew. A quote with no technical questions usually means the drawing was not read.
Step 3: Verify tolerance capability with evidence. Ask which tolerance applies to which feature, what inspection method proves it, and whether the number is process capability or a best-case record. Request a dimensional report from a comparable automotive or performance racing job.
Step 4: Confirm material and traceability. Ask for the mill certificate, the heat number, and whether substitution is ever permitted. For titanium, aerospace-grade aluminum and stainless grades this is non-negotiable for automotive performance applications.
Step 5: Order a paid prototype and inspect it yourself. Measure the critical features that matter, not the easy ones, and check edge quality, thread engagement, finish and flatness. A prototype that passes on your CMM removes most of the risk from the production order.
Step 6: Agree the inspection package up front. First article inspection report, dimensional report, material certificate, treatment certificate and packing photographs. Define AQL or full inspection for critical engine and suspension features before production, not after a rejection.
Step 7: Lock schedule, logistics and risk sharing. Confirm lead time from drawing approval rather than inquiry, agree what happens if material is delayed, and choose terms matching your risk: courier for samples, air freight for urgent prototype parts, sea freight for planned volume.
Step 8: Compare total cost, not unit price. A cheaper price with a weak first article, unclear documentation and unpredictable quality costs more in inspection labour, line stoppage and rework for high-performance automotive builds.
FAQ: Porsche-Grade CNC Machining Parameters and Capabilities
Each answer matches the parameter table above. Where a figure is quoted, the source is stated so your quality team can verify it independently.
Q1: Does Porsche AG Manufacture Cars Requiring CNC Machined Parts?
A1: Yes. Porsche AG manufactures high-performance sports cars, GT racing models, classic restoration vehicles and electric performance vehicles that rely heavily on precision CNC machined components. Five-axis CNC machining is widely used for engine housings, suspension parts, chassis fixtures and prototype components with ultra-tight tolerances.
Source: factory process capability list, November 2026; automotive precision machining standards.
Q2: Which materials are commonly used for Porsche CNC machined automotive parts?
A2: Aluminum 6061-T6, 7075-T6 and 2024; magnesium alloy; titanium alloy; stainless steel 303, 304, 316L and 17-4PH; brass C360 and copper C110; carbon steel 1045, 4140, 4340; and engineering plastics including POM, PEEK, PTFE, PA6 and UHMWPE. Material certificates are available on request, and substitution is never made without written approval.
Source: approved material list, factory quality manual.
Q3: What surface roughness and finishes are available for automotive performance parts?
A3: As-machined surfaces are typically Ra 6.3 μm, standard finishing reaches Ra 1.6 μm, fine finishing reaches Ra 0.8 μm, and grinding or lapping reaches Ra 0.4 μm. Treatments include anodizing Type II and Type III hard anodize, sandblasting, passivation, zinc and nickel plating, powder coating, laser marking and polishing.
Source: surface finish specification sheet; roughness tester measurement.
Q4: What is the minimum order quantity and is there a tooling charge for Porsche-style CNC parts?
A4: One piece is accepted for prototypes, classic spare parts and racing samples, and there is no tooling charge because CNC machining needs no dedicated mold or die. Programming and setup are priced into the quotation, so the second unit is far cheaper than the first.
Source: quotation policy, factory sales manual.
Q5: What is the maximum part size you can machine for automotive components?
A5: Milling up to 1200 × 800 × 500 mm and turning up to Ø400 × 1000 mm. Larger parts can sometimes be produced in split sections and assembled, but that changes tolerance stack-up and must be engineered rather than improvised.
Source: machine specification list, November 2026.
Q6: What lead time should I plan for automotive CNC prototype and batch parts?
A6: 5 to 7 working days for prototypes after drawing approval, and 12 to 18 working days for 100 to 1000 pieces. These figures assume material in stock and no special treatment; anodizing and plating typically add 2 to 4 working days, and imported material can add substantially more.
Source: production planning standard, November 2026.
Q7: Which drawing formats do you accept, and how are untoleranced dimensions handled for automotive drawings?
A7: STEP, IGES, X_T, DWG, DXF and PDF. Untoleranced dimensions follow ISO 2768-m by default, or ISO 2768-f where finer control is required, and geometric tolerances follow ASME Y14.5-2018. If your drawing uses another automotive standard, state it on the sheet, because the default assumption governs inspection and any dispute.
Source: ISO 2768-1:1989, ISO 2768-2:1989, ASME Y14.5-2018.
Q8: How is quality verified before shipment for automotive CNC parts?
A8: With a first article inspection report, a dimensional report against the drawing, material and treatment certificates, and CMM or vision measurement for positional and profile features. Hardness and roughness are checked with dedicated instruments.
Source: ISO 9001:2015 aligned quality control procedure; inspection equipment list.
Conclusion and Quote Request
You now have a working answer to Does Porsche AG Manufacture Cars Requiring CNC Machined Parts from a buying perspective: whether Porsche uses CNC components, which machining type fits each automotive geometry, which tolerances and finishes are realistic, how capability maps onto performance automotive applications, and how to qualify a supplier before you commit a purchase order.
If your project needs custom automotive precision CNC machining in metal or engineering plastic for racing, restoration or prototype vehicles, send your 2D drawing and 3D model with quantity, material, finish and target date. Our engineering team will review manufacturability, confirm the tolerance that applies to each critical feature, and return a quotation with lead time and inspection plan. No catalogue parts, no reselling, no vague promises: we machine what you specify and document what we ship.
Get In Touch
Ready to source precision CNC machined parts for your automotive project? Contact us today.
📄 Request a Technical Datasheet
Contact Us →📞 Speak with Our Engineering Team
Get In Touch →🔗 Browse Our Custom Battery Solutions
View Products →Dongguan A&S Power Technology Co., Limited.
315 PING 'AN AVENUE, PINGHU STREET, LONGGANG DISTRICT,
SHENZHEN CITY, GUANGDONG PROVINCE
📞 +86 18688963321
✉ samuel@chnzhongzhu.com
Stay Charged. Stay Connected.


What Is Better Polyamide Or Polyester?